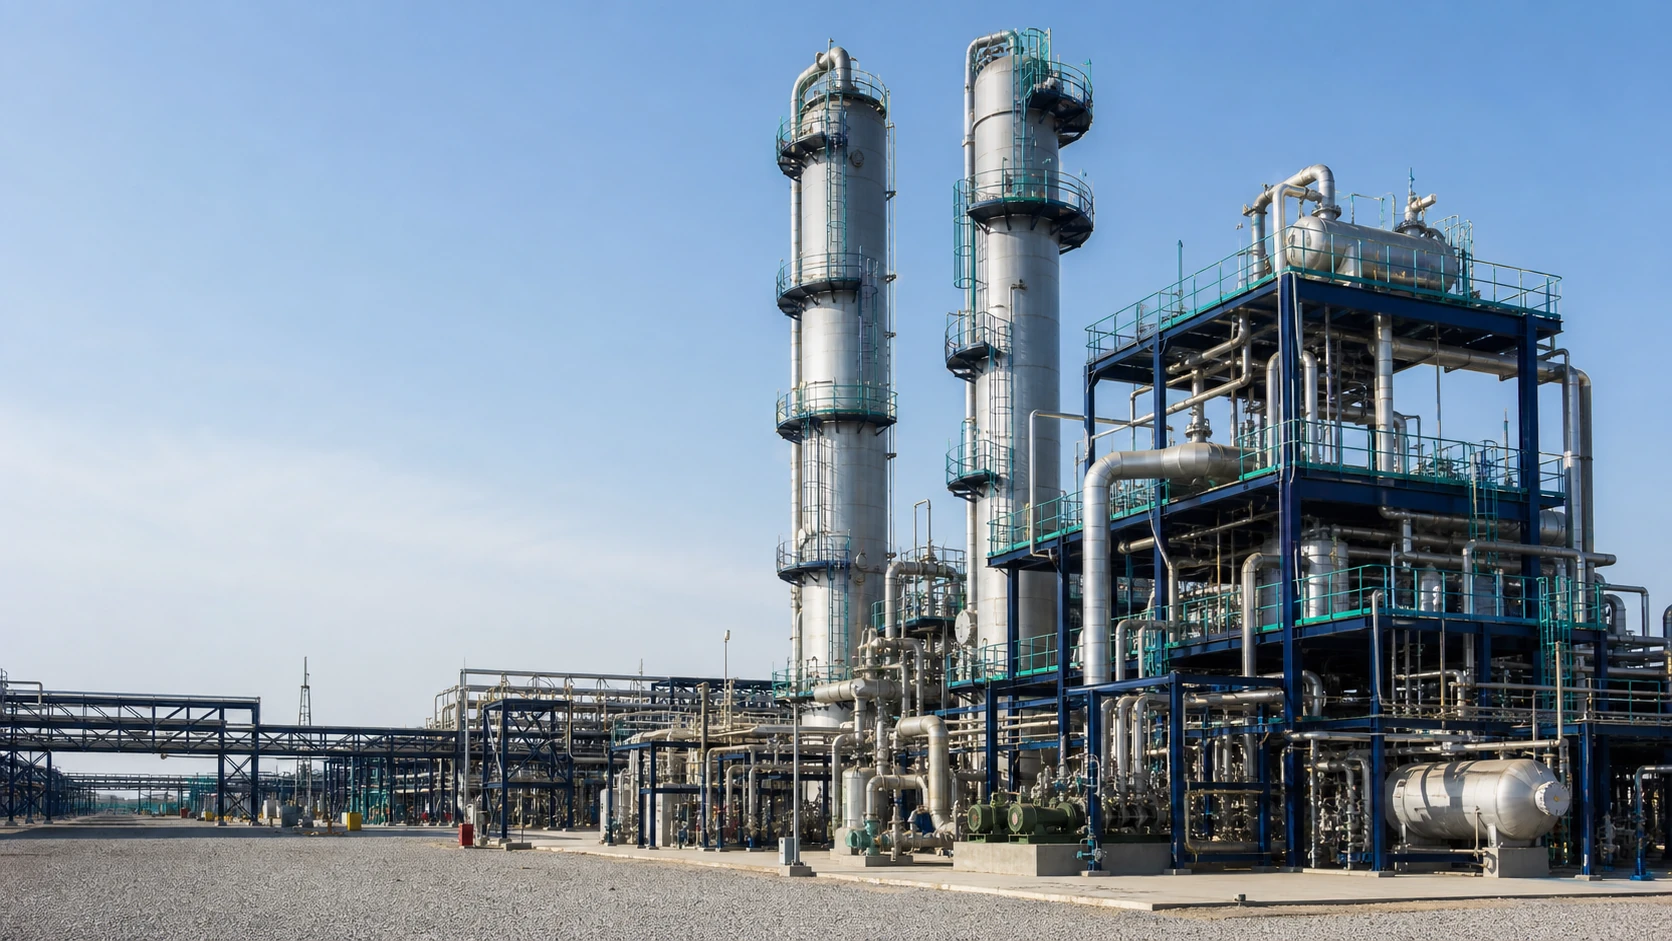
This technical page defines the engineering basis, supply boundaries and enquiry data for Gas Sweetening Units. Each project is configured around capacity, feed composition, product specification, ambient conditions, available utilities and the owner’s operating requirements rather than a fixed catalogue arrangement.
Engineering of Gas Sweetening Units concentrates on acid-gas removal targets, solvent selection and loading, absorber hydraulics, circulation rate, regeneration duty, solvent degradation, corrosion and sour-service safety. The selected configuration is verified against normal, minimum, start-up, shutdown and credible upset cases, then checked for operability, maintainability, energy use, process safety and site interfaces before the design is frozen.
Rated capacity, minimum stable load, feed envelope, inlet and outlet conditions, product specification, start-up and shutdown cases, design life and acceptance criteria are agreed before equipment definition is frozen. Process basis also fixes phase behaviour, contaminant loading, residence time, utility margins, separation targets, recycle or regeneration duty and the operating envelope for credible upset cases.
Mechanical design and materials
Materials, corrosion allowance, sour-service requirements, piping classes, nozzle design, insulation, coating, supports and maintenance access are coordinated with the actual process conditions and project code hierarchy.
Control, safeguarding and operation
Control philosophy, alarms and trips, cause-and-effect logic, interlocks, start-up and shutdown sequences, safe depressurization and operator access are developed consistently from the P&IDs through functional testing.
Layout, utilities and interfaces
Battery limits, tie-in points, structural loads, cabling, instrumentation, drains, vents, access routes, lifting envelopes and shipping constraints are controlled through coordinated models and interface drawings.
From project definition to delivery
Clear inputs and contract-ready outputs
Proposal quality depends on complete input data and an explicit acceptance basis. The following lists provide a practical starting point and are completed during technical clarification.
Recommended RFQ information
Feed flow, composition and credible operating envelope
Inlet conditions, required product specification and pressure-drop limit
Site and ambient data, hazardous-area classification and HSE requirements
Available utilities with pressure, temperature and capacity
Applicable standards, materials, supply limits and owner document formats
Typical engineering and supply deliverables
Design basis, heat and material balance, and process description
PFDs, P&IDs, equipment list and technical datasheets
Control philosophy, cause and effect, I/O definition and utility summary
Plot plan, 3D model, foundation loads and fabrication drawings
Inspection and test plans, FAT records, final data book and commissioning support
Delham Engineering
Define the scope around real project data
Send the available process data, battery limits and expected document list for a technical proposal. The engineering team will identify missing information through a structured clarification register.
A public manufacturer datasheet publishes the modular sizes below. These are reference values for amine-solvent circulation and package equipment only—not an industry-wide code limit, gas-feed capacity, or Delham rating.
Published values apply only to the cited equipment family and stated scope; they are not universal code limits or a Delham rating/guarantee.
Parameter
Published reference value
SI / secondary units
Application limit
Five-size modular amine-circulation series
10, 20, 40, 80 and 120 US gal/min
2.27–27.25 m³/h
Five published package sizes; this is solvent flow, not gas-feed flow.
Custom amine circulation
125–2,000+ US gal/min
28.39–454.25 m³/h
Published custom-design envelope; not a standardized series or guaranteed range.
Reboiler duty in the five-size series
0.75–5.5 MMBtu/h
220–1,612 kW
Reference-series duty; confirm heat source and project operating cases.
Contactor tower in the five-size series
OD: 18–30 in
OD: 457–762 mm; L: 52.5 ft (16.00 m); 20 trays
One published equipment family; not a universal tower-sizing rule.
Gas throughput and treated-gas limits
Project-specific
Not inferred from solvent circulation
Set from feed rate/composition, H2S/CO2 partial pressures, product specification and operating cases; agree acceptance criteria contractually.
Applicable pressure and temperature limits are established from the project design basis. The cited market reference does not publish a universal treated-gas flow rate; do not convert its US gal/min solvent figures to MMSCFD.